Crashes, No Sound, or Screen Glitches?
Random freezes, missing sound and display glitches usually trace back to one bad driver. Find and replace yours safely.Free scan · under a minutePC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Yes, you can build a small injection molding machine—but the realistic home-built version is a hand-powered or benchtop prototype machine, not a low-cost replacement for an industrial press. A DIY machine can be worthwhile for learning, recycling clean thermoplastic, prototyping simple parts, and making small repeatable objects. It becomes a poor choice when you need certified safety, tight tolerances, fast cycles, complex molds, or dependable production output.
The machine still has to perform the same essential jobs as a commercial press: heat thermoplastic into a controlled melt, force that melt into a closed mold, hold the mold shut while the part cools, and eject the finished piece. The difficult part is not making plastic hot. It is controlling heat, pressure, clamping force, electrical energy, fumes, and moving machinery without exposing the operator to serious injury.

As an Amazon Associate I earn from qualifying purchases.
What a DIY injection molding machine actually does
Injection molding starts with thermoplastic pellets or clean, identified flakes. The feedstock enters a heated barrel or chamber, melts, and is pushed through a nozzle or sprue into a mold cavity. The mold remains closed while the plastic cools and solidifies. It then opens so the part can be removed.
Commercial machines normally separate the process into two major assemblies:
#1 Best Overall
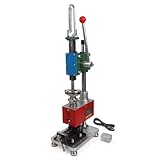
- Maximum Injection Amount (theoretical): 0-10g/time
- Cost Saving:This injection molding machine uses a simple hand-disassembled mold to complete the injection molding, and the mold can be replaced to achieve multiple uses of one machine. Furthermore, compared to pneumatic injection molding machines, it uses lower pressure and allows for the use of 3D printed molds to create products, making it suitable for DIY projects.
- Heating Temperature: 0-350°C(0~662°F). The temperature is adjustable according to material. PEPP temperature 200-240°C, ABS 180-210°C, PS 180-200°C
- The plastic injection machine comes with a test mold and bench vise. It can be used by connecting the power supply. Don't need to connect the air compressor. It is easy to use and simple to operate without take much space.
- Application: Soft plastics such as PP, PE, ABS are the most suitable, and PS, PA, PET, TPU, and PVC can also be used. Only a small amount of sample is needed for easy extrusion. Capable of small batch production and test
- The injection unit heats and moves the plastic.
- The clamping unit closes and holds the mold.
A compact DIY machine may combine these functions in a vertical frame, but combining them does not eliminate the requirements. The frame must resist the injection load, the barrel must contain hot plastic under pressure, and the clamp must prevent the mold halves from separating or moving unpredictably.
DIY machine versus industrial injection press
| Characteristic | Small DIY or recycling machine | Industrial or professional press |
|---|---|---|
| Power source | Often hand-powered or mechanically assisted | Typically hydraulic, servo-electric, or pneumatic-assisted |
| Process control | Limited temperature and force control; operator-dependent | Controlled injection speed, pressure, temperature, cooling, and cycle timing |
| Typical use | Education, recycling demonstrations, prototypes, and simple low-volume parts | Repeatable commercial production and demanding engineering parts |
| Mold complexity | Usually a simple two-part mold | May use slides, lifters, ejector systems, hot runners, and complex cores |
| Main limitations | Small shot size, slow cycles, inconsistent pressure, leakage, and operator exposure | Higher cost and complexity, but substantially better repeatability and guarding |
The distinction matters. A small machine may successfully demonstrate how recycled plastic flows into a mold while still producing parts with visible variation, flash, voids, warpage, or difficult ejection. It may teach the process more successfully than it produces saleable parts.
A documented starting point: Precious Plastic
The lowest-risk way to begin is to study a documented open-source design rather than independently inventing the heated barrel, pressure path, clamp, and control system. Precious Plastic’s official injection-machine reference describes a hand-powered machine intended to heat plastic flakes and inject them into a mold. The project presents it for small objects, prototyping, educational workshops, and small productions—not as a production-scale press.
Quick wins for a faster PC:
Clear out junk files and repair common Windows errorsFree Scan →Scan for outdated or missing drivers - takes under a minuteDriver Scan →Repair Windows errors before they cause bigger problemsFix Now →Its published reference data lists an approximately 30 kg machine measuring about 830 × 1,000 × 1,830 mm, with an 800 W, 230 V electrical system. These are design-reference figures, not guaranteed build specifications. They should not be treated as a United States cost or wiring recommendation. The project’s separate workspace information gives a Netherlands material-cost reference of approximately €250 for the injection machine and notes that a shredder is also needed for a recycling workspace. Actual cost varies substantially with local steel, heaters, controls, machining, electrical work, guarding, and mold construction.
Use the Precious Plastic injection machine documentation as a design reference and learning path. Before copying any drawing, confirm the current revision, material specifications, electrical requirements, and safety guidance. A plan is not a substitute for checking the finished machine.
Before cutting metal: define the part and process
Design the machine around one realistic part, not around the vague goal of molding “anything.” The part determines the shot size, mold dimensions, injection force, clamp load, ejection method, and cooling time.
A good first part is small, uncomplicated, and non-critical: a tag, tile, spacer, knob, tray, or low-load workshop accessory. Avoid undercuts, deep blind pockets, thin unsupported walls, tight cosmetic requirements, and features that require slides or unscrewing cores.
Recommended Free Tools
Make a simple process worksheet before building:
- Estimate the part volume.
- Add the volume of the sprue, runner, and any test excess to determine the required shot.
- Choose one known thermoplastic grade.
- Record the manufacturer’s melt-temperature, mold-temperature, drying, and residence-time guidance.
- Calculate or obtain an engineering estimate for the projected area of the part and the required mold-clamping force.
- Set a target mold size and opening direction.
- Decide how the part will be ejected without placing hands near the injection point or closing mold.
Clamping force is not something to guess from the size of the frame. A basic design relationship is projected area multiplied by expected cavity pressure, followed by an appropriate engineering safety factor. The actual pressure depends on the resin, flow length, wall thickness, gate, temperature, and injection system. If you cannot establish a defensible load estimate, do not rely on the machine for structural, pressure-containing, safety-critical, or commercial parts.
The essential machine subsystems
1. Rigid frame and base
Use a rigid steel or thick-wall aluminum structure that resists bending when the plunger loads the mold. The base should stand securely on a stable, noncombustible surface. A tall vertical design must be anchored or otherwise protected from tipping.
Check more than the strength of the material. Examine fastener engagement, joint slippage, weld quality, mold alignment, access for maintenance, and the load path from the plunger through the mold and into the frame. A frame that looks strong can still flex enough to cause flash, nozzle misalignment, or sudden mold movement.
2. Barrel, heated chamber, and nozzle
The barrel must provide a controlled path for feedstock and melt. It needs to withstand the intended mechanical and thermal loads, prevent plastic leakage, and connect securely to the nozzle and mold sprue. Do not assume that an ordinary thin tube, threaded fitting, or improvised plumbing component is suitable simply because it fits.
Use materials and connections selected for the temperature and pressure of the intended resin. The internal path should avoid dead pockets where old plastic can remain and degrade. A large barrel used for very small shots can also create excessive residence time, allowing the material to overheat before it is injected.
3. Heating and temperature control
The heating subsystem normally includes heater bands or cartridge heaters, a temperature sensor, a controller, wiring, a protected enclosure, grounding, overcurrent protection, and independent over-temperature protection. A temperature display alone is not a safety system.
A PID temperature controller with thermocouple may be part of a heating setup, but a marketplace controller is not automatically compatible with the heater wattage, sensor type, supply voltage, enclosure, or machine design. The control system should be reviewed by someone competent in mains electrical work. It should also have a means of disconnecting hazardous energy and a fault response if the sensor becomes disconnected or reports an implausible value.
Place the sensor where it measures the relevant barrel temperature rather than merely the temperature of a nearby heater band. Insulate or guard hot surfaces where appropriate, secure heater wiring against movement and abrasion, provide strain relief, and keep energized conductors inside a suitable enclosure.
4. Injection mechanism
The injection mechanism can be a hand lever, screw, mechanical plunger, pneumatic cylinder, hydraulic cylinder, or another assisted arrangement. It determines the available force, shot size, cycle time, and how close the operator must be to the hot zone.
Rank #2
A hand lever can be useful for demonstrations because it is simple and gives the operator direct feedback. It also makes pressure and fill time inconsistent. Pneumatic or hydraulic assistance can increase force, but it adds stored energy, hoses, valves, controls, and additional failure modes. More force does not make a weak frame, undersized nozzle, leaking mold, or inadequate guard safe.
5. Mold clamp
The mold must stay closed throughout injection and the early cooling period. The clamp should be mechanically stable and should not allow a mold half to fall, swing, or close under gravity while the operator is working nearby.
Design the clamp around the mold envelope, opening stroke, alignment, and calculated load. Include a positive method of securing the mold and a controlled opening action. Never hold mold halves together by hand during injection. Never reach into the mold area while the mechanism can move or while the mold and sprue are hot.
Free tools Windows power users keep installed
One-click scans. No signup required.
6. Guards, disconnects, and ventilation
Guard the mold-closing area, injection mechanism, hot barrel, nozzle, and hot sprue. A fixed guard or properly interlocked barrier should prevent access to pinch and crush points during operation. The emergency disconnect should remove hazardous energy without creating a new hazard, and it should be accessible without reaching through the danger zone.
Provide effective general ventilation and, where needed, local exhaust. Strong odor, visible smoke, or eye and throat irritation is not a normal process indicator. Stop the operation, isolate the energy, ventilate the area, and identify the material and cause before continuing.
Choose one known plastic first
Use clean, identified pellets or flakes for initial trials. Keep a written list of permitted materials and exclude unknown mixed plastics, coated materials, flame-retardant waste, contaminated feedstock, and any resin that the machine cannot heat and control reliably.
Known polypropylene injection molding pellets are a more repeatable starting point than unidentified household waste. The exact grade still controls the process window. Do not mix PP, HDPE, ABS, or other plastics merely because they look similar or melt at approximately the same temperature.
Do these 3 things before closing this tab:
1Clear out junk files and repair common Windows errors2Fix the driver behind crashes, sound loss and screen glitches3Repair Windows errors before they cause bigger problemsPolypropylene
PP is a practical candidate for a small machine because it is widely available and can produce durable parts. It is semi-crystalline and generally shrinks more than amorphous materials such as ABS, so mold design, cooling, and ejection deserve attention.
One LyondellBasell technical example for a particular filled PP grade lists a melt-processing range of approximately 220–260°C and a mold-temperature range of approximately 30–60°C, along with grade-specific drying requirements. Another example discusses processing around 450°F / 232°C. These figures demonstrate why the resin’s own technical data sheet must override generic internet settings; they are not universal PP temperatures.
PP can form useful integral hinges under the right combination of part design, gate placement, flow direction, and processing conditions. A basic DIY machine should not promise that result without testing.
HDPE and other polyolefins
Clean HDPE and other polyolefins may be suitable if the machine reaches the required melt temperature and the mold accommodates their shrinkage. Recycled material must be sorted and cleaned. Mixed grades, labels, dirt, moisture, and additives can cause inconsistent flow, odor, weak parts, and unpredictable dimensions.
ABS and engineering plastics
ABS can make rigid parts, but it usually benefits from more controlled heating, drying, venting, and processing than a simple hand-powered recycling machine provides. Polyamide, polycarbonate, PBT, PPSU, PPS, and other high-temperature engineering polymers are poor beginner materials for improvised equipment.
Some high-temperature materials require purpose-built plasticizing equipment, tight temperature control, drying, extraction, careful purging, and controlled residence time. Do not put a high-temperature polymer into a machine merely because the heater can reach its nominal melt temperature.
Moisture and residence time
Some resins are moisture-sensitive and must be dried before molding. Pellets from an open bag are not automatically ready to use. Follow the resin manufacturer’s drying temperature, time, and storage guidance. Overheating a polymer or leaving it in a hot barrel for too long can degrade the melt, produce discoloration or fumes, and leave degraded material in the flow path.
Purging also requires care. High-temperature purging can eject hot material unexpectedly, and some materials require a specified purge procedure. Never improvise a purge compound or temperature schedule for an unknown resin.
The Tool Desk
Outbyte Driver Updater FREEFix the driver behind crashes, sound loss and screen glitchesFind Drivers →Outbyte PC Repair FREERepair Windows errors before they cause bigger problemsFix Now →Design a simple first mold
The mold usually matters more than beginners expect. A powerful injection mechanism cannot compensate for a cavity that is difficult to fill, impossible to vent, or designed so the part locks itself inside.
Rank #3

- Used Book in Good Condition
For a first project, use a two-plate mold with a clear parting line and a cavity that opens without forcing the part to remain on the wrong half. Aluminum is practical for low-volume molds because it is comparatively easy to machine and transfers heat effectively. Aluminum mold blocks and mold-making tools are directly useful here, but the material alone does not guarantee a good mold; accurate layout, machining, alignment, venting, and surface finish still matter.
Parting line and draft
Choose the parting line so that the mold halves separate cleanly and the finished part can be removed without scraping or prying against delicate features. Add draft to surfaces parallel to the opening direction. The required draft increases with cavity depth, surface texture, shrinkage, and the tendency of the resin to grip the mold.
Insufficient draft can cause stuck parts, whitening, gouging, damaged edges, and excessive force during ejection. If you need aggressive draft removal, sliders, lifters, or a complex ejector system for the first part, redesign the part instead.
Gate, runner, and sprue
Provide a defined sprue or runner path from the nozzle to the cavity. Gate into a thicker section where possible so the flow has a better chance of filling the part and feeding shrinkage. Keep the flow path as short and uncomplicated as the part permits.
Gate location affects weld lines, visible marks, filling pressure, fiber orientation in filled materials, and the direction of shrinkage. A part that fills from the wrong location may require much more force than the machine can provide.
Vents and ejection
Add vents at the end of the flow path and in areas where air is likely to become trapped. Poor venting can produce short shots, burn marks, dark specks, or compressed air pockets. Do not solve a venting problem by simply increasing temperature or force.
Plan how the part, sprue, and runner will be removed. A simple part may release by hand after cooling, while a more complicated part may need ejector pins or a stripper feature. Keep ejection forces aligned with the mold and never use a hand tool in a hot, energized, or movable mold area.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
A welded mold can be useful for rough recycling demonstrations, but weld distortion, leakage, poor venting, and difficult demolding can limit quality. For a first useful mold, prioritize easy opening, accurate alignment, and reliable venting over intricate geometry.
A staged build and commissioning sequence
Do not build the machine and immediately load it with plastic. Treat commissioning as a series of gates. If a gate fails, correct the problem before moving to the next one.
Stage 1: document the design
- Draw the complete load path from the injection mechanism through the mold and frame.
- Identify every hot surface, pinch point, crushing point, electrical enclosure, and stored-energy source.
- Specify the resin grades, temperature range, maximum shot, mold envelope, and intended operating cycle.
- Decide where guards, emergency disconnects, access doors, and ventilation will be installed.
- Have the structural and electrical portions reviewed by appropriately qualified people.
Stage 2: cold mechanical checks
With no heat and no polymer, check frame deflection, fastener engagement, clamp travel, mold alignment, nozzle-to-sprue alignment, lever or cylinder travel, and the behavior of every moving component. Confirm that the mold cannot close unexpectedly when the operator is loading or removing a part.
Stage 3: electrical and control checks
Before energizing the heater, verify grounding, insulation, overcurrent protection, wiring ratings, strain relief, control-enclosure integrity, emergency disconnect operation, sensor placement, and over-temperature protection. A qualified person should perform or review mains-voltage work. Confirm that a sensor fault or controller failure cannot leave the heater running without a safe limit.
Stage 4: controlled heat-up
Follow the heater and controller manufacturer’s instructions for the first heat-up. Monitor the barrel and surrounding surfaces rather than relying only on the controller display. Stop if temperatures overshoot, rise unevenly, wiring softens or moves, insulation smokes, or plastic residue begins to decompose.
Stage 5: first shots
Use one known resin and the lowest practical temperature and injection force that can fill the test cavity. Keep people away from the mold parting line and nozzle. Start with short, controlled shots and allow sufficient cooling before opening the mold.
Record the resin grade, lot or source, moisture condition, barrel temperature, mold temperature, injection force or lever setting, fill time, cooling time, part mass, visible defects, and any unusual odor or ejection behavior. Change one variable at a time. Without records, it is difficult to distinguish a material problem from a mold, temperature, venting, or clamping problem.
Common defects: diagnose the process, not just the symptom
| Defect | Possible causes | Useful first checks |
|---|---|---|
| Short shot | Insufficient melt volume, low melt or mold temperature, restricted gate, poor venting, excessive flow length, or insufficient injection force | Check shot calculation, resin guidance, gate and vents, nozzle alignment, and whether the machine is losing force through frame flex or leakage |
| Flash | Insufficient clamp force, excessive injection or packing force, damaged mold faces, parting-line gaps, or an overfilled shot | Inspect mold faces and alignment before increasing clamp force; do not treat flash by adding uncontrolled pressure |
| Sink marks or voids | Uneven wall thickness, inadequate packing, hot spots, insufficient cooling, or shrinkage in thicker sections | Review wall design, gate location, cooling time, and temperature uniformity |
| Warping | Nonuniform cooling, uneven wall thickness, flow orientation, mold-temperature differences, or premature ejection | Allow more cooling, inspect the mold for temperature differences, and redesign abrupt thickness changes |
| Burn marks or dark material | Trapped air, excessive temperature, excessive residence time, degraded material, or contaminated feedstock | Check vents, resin identity, barrel residence time, and temperature before attempting a hotter or faster shot |
| Part sticks in the mold | Insufficient draft, rough cavity, poor parting-line choice, inadequate ejection, or excessive shrinkage onto the core | Improve draft and ejection design; do not pry against a hot cavity or reach into a movable mold |
Defects rarely have only one possible cause. Material, temperature, gate design, pressure, cooling, mold geometry, and venting interact. LyondellBasell’s processing guidance emphasizes the effects of nonuniform cooling and part geometry on shrinkage and warpage, while BASF provides material-specific troubleshooting information for injection-molding problems.
The Tool Desk
Outbyte Driver Updater FREEScan for outdated or missing drivers - takes under a minuteDriver Scan →Outbyte PC Repair FREEClear out junk files and repair common Windows errorsFree Scan →Rank #4
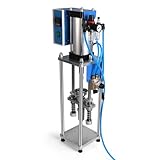
- Maximum Injection Amount (theoretical): 0-20g/time
- Cost Saving:This injection molding machine uses a simple hand-disassembled mold to complete the injection molding, and the mold can be replaced to achieve multiple uses of one machine.
- Heating Temperature: 0-350°C(0~662°F). The temperature can be adjusted. PEPP temperature 200-240°C, ABS 180-210°C, PS 180-200°C
- Pneumatic Plastic Extruder: You need to prepare the air pump, and a 30L 500W or higher power air pump is recommended, and the air pressure requirement is between 0.65-0.85
- Application: Soft plastics such as PP, PE, ABS are the most suitable, and PS, PA, PET, TPU, and PVC can also be used. Only a small amount of sample is needed for easy extrusion. Capable of test piece production and small batch production.
Safety is part of the machine design
This machine combines hot polymer, electrical power, stored mechanical energy, and crushing motion. The possible injuries include serious burns, electrical shock, cuts, avulsions, amputations, and fire.
U.S. OSHA plastics-machinery guidance identifies high voltage, high temperature, nip points, moving components, burns, cuts, avulsions, and amputations as hazards. Oregon OSHA’s point-of-operation guidance likewise identifies crushing, avulsion, amputation, and severe burn risks around injection-molding machinery. The exact legal requirements depend on jurisdiction, whether the machine is used at home or in a workplace, and how it is operated, but the physical hazards exist everywhere.
Use the following as a minimum design and operating checklist:
- Install fixed or interlocked guarding around the mold-closing and injection danger zones.
- Guard heater bands, the hot barrel, nozzle, sprue, and other surfaces that can burn an operator.
- Prevent the clamp or mold half from falling or closing under gravity.
- Provide an accessible emergency disconnect and a clear shutdown procedure.
- Use proper grounding, overcurrent protection, appropriately rated wiring, protected terminals, and a suitable control enclosure.
- Use lockout/tagout or an equivalent documented isolation procedure before cleaning, clearing a jam, changing a mold, or servicing the machine.
- Wear eye protection and, where splash or ejection is possible, a face shield. Use task-appropriate heat-resistant gloves, long sleeves, and closed footwear.
- Heat-resistant molding gloves and other PPE can reduce exposure, but PPE never replaces guarding, electrical protection, training, or safe isolation.
- Provide effective ventilation or local exhaust and stop immediately if the process produces smoke, strong odor, or irritation.
- Keep a written list of approved resins and exclude PVC, unknown mixtures, and contaminated waste.
- Keep a suitable fire extinguisher available and ensure operators know how to disconnect the machine safely.
The ANSI/PLASTICS B151.1 standard is a relevant professional reference for horizontal and vertical clamp injection molding machines. The current standard may require purchase or authorized access, so consult the applicable edition and a qualified safety professional rather than assuming that a home-built machine meets it.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
When buying is the better construction decision
Building is sensible when the primary goal is learning, experimentation, recycling education, or a small number of forgiving parts. Buying or outsourcing is usually more sensible when you need repeatability, documented guarding, reliable cycle times, or a part that must meet a specification.
A benchtop plastic injection molding machine is not automatically safe or suitable, but comparing one with a DIY build can expose hidden costs. Check its voltage and electrical requirements, clamp force, shot size, mold envelope, temperature zones, guard design, emergency controls, documentation, replacement parts, and service support. Compare the complete installed cost of the machine—not just the frame and heater—with the cost of steel, machining, controls, wiring, mold-making, guarding, ventilation, testing, and your own time.
Outsource the mold or the entire prototype when you need tight tolerances, complex features, a better surface finish, or dependable repeatability. A professional injection mold machining or rapid molding service can also provide a design-for-moldability review before you spend more time modifying a machine that cannot meet the requirement.
What this machine should not make
Do not use DIY-molded parts for medical, food-contact, pressure-containing, structural, load-bearing, electrical-safety, or life-critical applications unless the complete material, mold, process, testing, traceability, and certification requirements have been addressed. A part’s appearance does not establish its strength, cleanliness, dimensional stability, or regulatory suitability.
Crashes, No Sound, or Screen Glitches?
Random freezes, missing sound and display glitches usually trace back to one bad driver. Find and replace yours safely.Free scan · under a minutePC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11For construction work in particular, do not substitute an untested molded part for a rated bracket, fastener, guard, connector, lifting component, pressure fitting, or other component whose failure could injure someone or damage property.
Practical capability checklist
A home-built machine is ready for limited, supervised prototyping only when you can answer “yes” to all of these questions:
- Is the intended resin identified, clean, and supported by the machine’s temperature and ventilation controls?
- Can the barrel, nozzle, frame, injection mechanism, and mold withstand the intended thermal and mechanical loads?
- Can the clamp hold the mold closed without relying on the operator’s hands?
- Does the mold have a practical parting line, draft, gate, vents, alignment, and ejection method?
- Are hot surfaces, pinch points, crush points, and energized conductors guarded?
- Are grounding, overcurrent protection, emergency disconnect, and over-temperature protection verified?
- Can the machine be isolated safely for cleaning, mold changes, jams, and maintenance?
- Is ventilation adequate for the chosen material and any purging operation?
- Can you record process conditions and repeat a result rather than relying on memory?
- Are the resulting parts restricted to low-risk uses until they have been properly tested?
If any answer is “no,” the next step is not a hotter heater or a stronger lever. Correct the design, obtain a professional review, choose a simpler mold and resin, or use a commercial machine or molding service.
Reference note: The technical basis for this guide includes the Precious Plastic injection-machine and workspace references, U.S. OSHA plastics-machinery guidance, Oregon OSHA point-of-operation guidance, ANSI/PLASTICS B151.1 as a professional safety reference, LyondellBasell polypropylene processing guidance, and BASF polymer-processing documentation. Requirements and product availability vary by location and date.
Frequently Asked Questions
Is building an injection molding machine cheaper than buying one?
It can be cheaper for a basic educational or recycling machine, especially when existing workshop equipment and scrap materials are available. The comparison changes once you include machining, electrical controls, guarding, ventilation, mold construction, testing, and your time. A commercial benchtop machine may be the better value when repeatability and support matter.
What plastic is best for a first DIY injection-molding project?
Use one clean, identified thermoplastic grade and follow its technical data sheet. PP or HDPE can be practical candidates for a small machine, but neither should be treated as a universal setting. Avoid PVC, unknown mixed waste, contaminated plastics, and high-temperature engineering polymers until the equipment and process controls are purpose-built for them.
Can recycled plastic flakes be used directly?
Only when the material has been sorted, cleaned, identified, and processed within a known temperature and safety window. A recycling workspace may also require a separate shredder. Household plastic that merely looks like PP or HDPE is not reliably identified and may contain incompatible polymers, coatings, additives, moisture, or contaminants.
What is the most dangerous part of a DIY injection molding machine?
There is no single hazard. The combination of a hot barrel and molten polymer, mold-closing and injection pinch points, stored mechanical energy, mains electricity, and fumes creates the risk. Guarding and energy isolation are more important than simply wearing gloves or installing a temperature display.
Quick wins for a faster PC:
Clear out junk files and repair common Windows errorsFree Scan →Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Repair Windows errors before they cause bigger problemsFix Now →The Bottom Line
A DIY injection molding machine is a worthwhile workshop project when you treat it as a controlled prototype and recycling tool. Start with a documented design, one known resin, one simple two-part mold, and a staged commissioning process. Build guarding, electrical protection, ventilation, and safe isolation into the machine from the beginning. For production, complex molds, tight tolerances, or safety-critical parts, buy a properly engineered press or use a professional molding service instead.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.




