Do these 3 things before closing this tab:
1Clear out junk files and repair common Windows errors2Fix the driver behind crashes, sound loss and screen glitches3Repair Windows errors before they cause bigger problemsIf you are using a filament (FDM/FFF) 3D printer, the fastest way to diagnose a failed print is to note where it failed. A first-layer failure usually points to the build plate, nozzle height, speed, or extrusion. Gaps that appear later suggest moisture, a clog, heat creep, or a feed problem. Lifted corners indicate thermal stress, while sideways shifts and “spaghetti” usually mean the part moved, collapsed, or was not adequately supported.
Most recurring failures fit five practical categories: first-layer adhesion, incorrect cooling or temperature, wet filament, inconsistent extrusion, and a model or mechanical problem. Start with the smallest adjustment that tests the most likely cause; do not change temperature, speed, cooling, flow, retraction, and supports all at once.
As an Amazon Associate I earn from qualifying purchases.
Quick symptom-to-cause guide
| What you see | Most likely causes |
|---|---|
| Filament will not stick | Dirty plate, incorrect Z offset, leveling, temperature, speed, or poor extrusion |
| Corners lift or layers crack | Warping, drafts, excessive cooling, insufficient bed heat, or too little contact area |
| Bubbles, popping, or rough surfaces | Moist filament, though temperature and extrusion problems can look similar |
| Gaps or missing layers | Partial clog, heat creep, feed resistance, low temperature, low flow, or wet filament |
| Layers shift sideways | Collision, loose belt or pulley, obstruction, excessive acceleration, or skipped steps |
| Spaghetti | Detached part, failed support, collision, collapsed geometry, or an inadequate model |
1. The first layer is failing
The first layer determines whether the rest of the print has a stable foundation. Typical symptoms include filament curling around the nozzle, lines remaining separate, corners lifting immediately, the nozzle scraping the plate, or plastic being deposited in mid-air.
Quick wins for a faster PC:
Repair Windows errors before they cause bigger problemsFix Now →Scan for outdated or missing drivers - takes under a minuteDriver Scan →Clear out junk files and repair common Windows errorsFree Scan →Work through these checks
- Stop and inspect the build plate. Remove old filament and debris, then clean the surface according to its manufacturer’s instructions. Avoid touching the active area with bare fingers. Confirm that the flexible sheet or plate is fully seated, flat, and undamaged.
- Run the printer’s leveling or first-layer calibration routine. Bed leveling, Z offset, plate cleanliness, and plate installation are separate issues. A level bed cannot compensate for grease, a loose sheet, or an incorrect first-layer height. Menu names vary by printer and firmware. On Prusa machines, first-layer calibration and live Z adjustment are key controls; lowering Z too far can damage the sheet or cause excessive vibration. See Prusa’s first-layer guidance.
- Slow the first layer. As a diagnostic starting point, try roughly 75% of the normal speed for the first layer or first few layers where your printer allows live adjustment. This is not a universal permanent setting.
- Use the filament manufacturer’s temperature range. If adhesion is nearly successful, test a bed-temperature increase of about 5–10°C. Change only that variable and record the result. Continually increasing heat can cause elephant’s foot, softening, or deformation.
- Add contact area when necessary. A brim can help narrow, tall, or corner-prone parts stay attached. It improves mechanical contact but will not fix a dirty plate, incorrect calibration, a damaged surface, or an incompatible material-and-plate combination.
If the nozzle is correctly positioned but little or no plastic comes out, stop recalibrating the bed. Check the filament path, nozzle, and extruder instead.
#1 Best Overall

- Durable, rigid construction; Solid rivets keep the blades in place, no more repurposed artist palette spatulas with spinning, twisting and turning cramp rings!
- Long knife with a beveled front edge; Slides very gently underneath prints with ease to protect the build bed surface yet provides good reach and allows prying
- Stiff, hardened stainless steel blades; Flexible but not too thin or flimsy, safer rounded edges, work well with different size objects without damaging them
- Stylish and useful; The smaller offset spatula has a black ergonomic rubber comfort grip, the knife has a big thick wood handle suitable for larger parts
- Essential addition to your 3D Printer accessories; No more putty knives to remove prints. Doubles as a leveling tool to scrape off stuck-on plastic from the print bed
2. The material is cooling or shrinking incorrectly
Warping occurs when printed material cools unevenly and contracts. It is especially common on large footprints and with higher-temperature materials such as ABS, ASA, polycarbonate, and some nylon or composite filaments. Corners may lift from the plate, or cracks may appear between layers.
Start with the manufacturer’s material profile, then make small, controlled changes:
- Keep the build plate clean and properly heated.
- Reduce drafts and sudden room-temperature changes.
- Use a brim or small “mouse ears” on vulnerable corners.
- Use an enclosure or controlled chamber when the material requires one.
- Reduce part cooling for materials that need a warm environment and slower cooling.
- For small overhangs and isolated details, use enough fan cooling to prevent deformation without cooling the entire part excessively.
- Slow the print when layer bonding is poor or the part is large and thermally stressed.
Do not treat “increase the fan” or “turn the fan off” as universal advice. PLA generally benefits from substantial cooling after the first layers. ABS and ASA usually need reduced drafts and a warmer environment. PETG needs a balance between overhang cooling, bonding, and stringing. Nylon, polycarbonate, and composite filaments may require drying, an enclosure, a specialized surface, or a more precise profile. Prusa’s warping guidance explains why excessive cooling can lift an object and reduce layer adhesion.
3. The filament is wet
Many FDM materials absorb moisture from the air. Wet filament can produce stringing, oozing, popping, bubbles, blobs, rough surfaces, weak layer adhesion, and inconsistent flow. TPU, nylon, PVA, BVOH, polypropylene, and some composites are particularly moisture-sensitive, but PLA and PETG can also develop problems.
Rank #2

- Precise measurement: Measurement range: 0 - 6''/0 - 150 mm; Resolution: 0.01”/0.1 mm; Accuracy: +/- 0.2 mm/0.01”. Perfect and accurate caliper measuring tool for household/DIY measurement
- 4 measuring modes: This digital caliper can be used to Measure inside and outside diameter, depth and step with two sets of jaws and a probe
- Inch/mm conversion: One button quick switch between two units: inch and millimeter, definitely save your time. The buttons are made of rugged plastic carbon fiber composites, durable and portable
- Zero setting function: The smart design allows you to set zero with an easy touch of a button and start a new measurement at any point of the scale, ideal for differential measuring
- Large LCD screen & auto off: The large and easy-to-read LCD display helps you get precise results quickly and easily, auto shutdown for saving battery after 5 minutes if without operation
A spool that was just opened is not guaranteed to be dry. Packaging may have been compromised, or the filament may have absorbed moisture after opening. Test the theory with a freshly opened, properly stored spool. If it prints cleanly while the older spool pops, bubbles, or produces rough surfaces, moisture is a strong suspect.
Dry and store it safely
- Check the filament manufacturer’s specified drying temperature and duration.
- Use a purpose-built filament dryer or a verified low-temperature drying method.
- Let the spool cool in a dry environment.
- Store it in an airtight container or dry box with fresh desiccant.
- Feed highly moisture-sensitive materials directly from a dry box where practical.
Do not assume a kitchen oven is safe. Household ovens may not hold a sufficiently low temperature accurately, risking deformation or damage to the spool and filament. Follow the material manufacturer’s drying instructions.
Moisture and clogging can overlap. Wet filament more often causes popping, bubbles, stringing, and roughness; a clog or feed problem more often causes little or no extrusion, increasing gaps, extruder clicking, a weak or curled stream, and failure that worsens during the print. A known-dry spool is a useful test before replacing hardware.
Recommended Free Tools
4. Extrusion is inconsistent
Gaps and missing layers are symptoms of under-extrusion, not proof of a clogged nozzle. Possible causes include a partial clog, contaminated filament, heat creep, a tangled spool, excessive resistance in the spool holder or PTFE path, incorrect filament diameter or material profile, incorrect extruder-idler tension, worn drive gears, an abrasive-filament-worn nozzle, low printing temperature, low flow, or moisture.
Rank #3

- General all-purpose cleaning kit helps you to remove the dirty partsoff your 3D Printers, keeps your 3D Printers performing at their best
- Double-ended, or single ended metal picks, 6.7 Inch long at most.
- Lots of different tips to find the right tool for the job. They work great to help clean/pick 3D printed parts, suitable for daliy repair.
- With a wide variety of shapes and sizes of the pics, it is easy to get into the small groups and clean like it’s never been cleaned before
- Please note that the picks is easy to small and sharp.
Use this recovery sequence
- Check the spool. Make sure it turns freely and has no crossed loop or knot. Confirm that filament is not rubbing against the frame, holder, or enclosure.
- Purge in a controlled way. Heat the nozzle to the appropriate temperature for the loaded material and extrude a short length. The stream should be steady and reasonably straight. Do not push cold filament through a hotend unless the manufacturer specifically instructs you to do so.
- Inspect the filament path and drive gear. Dust, filament shavings, or a ground-down section of filament can indicate slipping or excessive resistance.
- Clear the nozzle using the printer’s procedure. Depending on the model, that may involve cleaning filament, a cold pull, a needle, or nozzle replacement. Tools and insertion depths are model-specific. For supported Prusa models, the manufacturer describes an approximately 0.3–0.35 mm wire or acupuncture needle inserted roughly 1–2 cm from below; do not generalize that instruction to every hotend. See the relevant manufacturer procedure.
- Check for heat creep. A hot enclosure, warm room, obstructed heatsink, failed hotend fan, or unsuitable cooling configuration can soften filament too high in the hotend. The printer may continue moving while extrusion gradually stops. Prusa identifies heat creep as a possible cause of extrusion stopping mid-print.
- Replace the nozzle if necessary. If cleaning does not restore a consistent stream, replacement may be safer than repeatedly forcing tools through a damaged or hardened nozzle. Confirm the nozzle diameter and material profile in the slicer afterward.
Never keep increasing temperature indefinitely to melt through a clog. The safe maximum is limited by the hotend, heater, thermistor, heatbreak, filament, and printer firmware.
5. The model moved or the sliced toolpath is inadequate
Layer shifts and spaghetti failures often involve the part, supports, slicer, or printer mechanics rather than a single temperature setting.
When layers shift sideways
If every layer shifts in the same direction, inspect belts, pulley grub screws, mechanical obstructions, acceleration, and skipped motor steps. If the shift occurs immediately after an impact, look for a warped corner, detached support, nozzle collision, or infill that rises above its intended layer. A collision can cause the motor to skip steps and permanently move the toolhead or bed relative to the sliced path.
Free tools Windows power users keep installed
One-click scans. No signup required.
Also inspect the gantry, rods, wheels, or rails for binding. Excessive speed or acceleration can overwhelm a machine, especially when the nozzle collides with a curled overhang, detached support, or warped section.
Rank #4
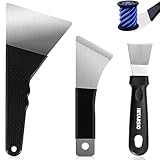
- 【3D Printer Removal Tools 3-IN-ONE Kit, 2-Year Warranty】Selected by a 15-Year 3D print enthusiasts team, We believe that pairing each model with the right scraper leads to expert results. This removal kit includes ③x differnet types of tools to prevent 3D printer bed damage such as scratches, residue buildup, 3D prints deformation, while enhancing 3D printing efficiency and improving models removal quality. Offers pro-level tools at outstanding value - no premium price needed.
- 【Large Removal Scraper, Edge Precision-Sharpened to 0.4mm】This Large Removal Spatula features a thinner, larger, and sharper edge design (ONLY 0.4mm in blade thickness, 3.94 inches in blade length) compared to standard removal tools. The scraper bends up to 60° and quickly returns to shape. Made of stainless steel, it performs exceptionally well on larger 3D prints such as 3D printed dragon egg, 3d printed castle etc.
- 【Medium Removal Scraper, Edge Sharpen to 0.55mm】The medium spatula whole tool is made from C45 steel, making it strong and durable (0.55mm in blade thickness, 2.36 inches in blade length). The scraper features an anti-slip grip for comfortable use. Great for 3D printed projects for example 3D printed toys etc
- 【Small Removal Scrapers, Edge Sharpen to 0.5mm】The removal scraper features a 15-degree angle (0.5mm in blade thickness, 1.57 inches in blade length), providing optimal leverage and precision, removing parts from the print bed without disturbing other prints or structures. Perfect for scraping 3D printed small animals, decorations, miniatures etc.
- 【Great 3D Printer Accessories Gifts】Designed for removing prints of various sizes without damaging the printer bed, this kit includes everything 3D printing enthusiasts and beginners need for fast and efficient separation. It is perfect for models of all sizes. It can effectively remove filament prints made of ABS, PLA, PETG, etc. INTARSIO Promise: All products come with a 2-Year warranty and all questions will be answered by our friendly customer service team within 12 hours.
When the print becomes spaghetti
Spaghetti means the printer is extruding into empty space because the intended geometry is no longer where the slicer expected it to be. The first layer may have detached, a support may have failed, the model may have collapsed, or a collision may have moved the part. Prusa describes this as filament being deposited in the wrong place after the object moves or collapses.
Before printing, preview every layer in the slicer. Check the first layer, support interface, thin walls, isolated islands, and overhangs. Repair non-manifold or corrupted meshes, reorient the model to reduce unsupported geometry, and add supports where the shape genuinely requires them. A brim can stabilize tall or narrow parts, but it cannot replace adequate support for an overhang.
Verify the selected printer, nozzle diameter, filament, bed profile, and material profile. A current printer troubleshooting index such as Prusa’s troubleshooting guide separates layer shifting, warping, and other failure categories because “spaghetti” is a symptom, not a single diagnosis.
A 10-minute recovery checklist
- Clean and reseat the build plate.
- Confirm the correct printer, nozzle, filament, and bed profile.
- Check that the spool rotates freely and the filament path is clear.
- Run the printer’s first-layer calibration.
- Slow the first layer for a controlled test.
- Test with a known-dry spool.
- Purge and inspect the extrusion stream.
- Preview the sliced model layer by layer.
- Add a brim or supports if the geometry needs them.
- Inspect belts, pulleys, rails, fans, and obstructions if layers shift.
Change only one or two variables at a time. If you alter Z offset, nozzle temperature, bed temperature, speed, cooling, flow, retraction, and supports together, you may get a successful print without learning which cause was responsible.
Best Value

- 【Upgraded 68-in-1 3D Printer Tools Kit, 1-Year Warranty】Designed by a Team of 15-Year 3D Printing Enthusiasts, the kit includes all essential tools. From wire cutters to needle-nose pliers, it cuts and trims PLA and other filaments precisely and fast. From high-quality hand drill with 10 drill bits to 5 types of metal files, your 3D printing range expands to a wide variety of materials. Upgraded durable 900D Oxford fabric with orange tags for quick and easy organization.
- 【Scrapers for Flawless Removal 3D Printed Models】One Stainless Steel removal scraper features a 15-degree angled (0.5mm thickness, 1.57-inch length), providing optimal leverage and precision, perfect for models like 3D printed dragon eggs and ideal for PETG, ABS, PLA+. The smaller orange scraper, with 10 extra-thin flat blades, offers pinpoint accuracy, making it ideal for removing small models with precision, such as 3D printed toys.
- 【1 Deburring Tool & 10 HSS BS1010 Swivel Blades】Our model polishing tools include 3 engraving knives with 9 types of blades, 5 different metal files and a 360° swivel-head deburring tool. This deburring tool conforms to uneven shapes, surfaces, edges, and ideal for PETG, ABS, PLA+ 3D printed models. Additionally, we add 10 EXTRA razor-sharp BS1010 blades made of tempered high-speed steel. HSS is known for being stronger and lasting 80% longer than regular steel.
- 【Nozzle Cleaning Needles, Brushes & Tweezers】To avoid inconsistent filament extrusion caused by a clogged nozzle, we provide 5 types of cleaning needles, (0.2mm, 0.25mm, 0.3mm, 0.35mm, 0.4mm), suitable for most 1.75mm PLA/ABS filament 3D printers. 3 Different cleaning brushes — made of Brass, Stainless Steel and Nylon for different cleaning conditions. Bent, Straight, Flat-Tip tweezers are added for precision cleaning.
- 【3D Printer Accessories Gifts Must-Have】4 cut-resistant finger cots to protect your fingers while working. A black sleeve case makes it easy to find, organize, store, and transport your tools. It keeps all 3D printer tools in excellent condition by protecting them from dust, debris, and moisture —ensuring all tools stay sharp and ready for your next 3D printed task. Your Satisfaction, Our Promise: All products come with 1-YEAR warranty and all questions will be answered within 12 hours.
When to service or replace hardware
Stop treating the problem as a slicer adjustment when you have persistent under-extrusion with a verified dry spool and clean nozzle, repeated layer shifts after tightening and obstruction checks, a failed hotend fan, temperature-sensor errors, or a damaged build plate, nozzle, belt, pulley, or heatbreak.
Also stop and follow the printer manufacturer’s safety procedure for an unusual electrical smell, uncontrolled heating, or a thermal-runaway warning. Do not continue unattended printing while a hardware fault is suspected.
Buy only the part that matches the diagnosis
A known-good spool is often the cheapest diagnostic tool. A dryer is appropriate when moisture symptoms are present; a dry box mainly prevents reabsorption and does not necessarily dry a saturated spool. A replacement build plate makes sense when the existing surface is worn, damaged, contaminated beyond cleaning, or unsuitable for the material—but it must match the printer’s dimensions, thickness, magnetic system, surface type, temperature limits, and material compatibility.
Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchWindows Errors? Fix Them Before They Spread
Repair common Windows errors and clear accumulated junk for a smoother, more stable PC - no reinstall needed.Free scan · no reinstallReplacement nozzles must match the printer family, thread, length, heatbreak geometry, tool requirements, and material. Brass may be suitable for ordinary PLA, while abrasive composites may require a hardened nozzle. After changing diameter, update the slicer profile. Do not assume a more expensive filament or accessory will solve a calibration, clog, tangle, or model-design problem.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

