PC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchKerf is the width of material a cut removes. It is not always the nominal width of a saw blade or laser spot, and there is no one figure that applies to every cutter. The effective kerf depends on the tool, material, thickness, condition and settings. For an accurate fit, make a test cut with the setup you intend to use, measure it, and account for that measured width in your layout.
What is kerf?
Kerf is the width of the strip of material removed by a cutting process. With a saw, the cut may be wider than the blade plate because the teeth are set outward. Haas defines kerf in its HAB operator manual as the blade’s cut width including the tooth offset.
With a laser, the beam removes material on both sides of its path. As Rob, an author on BRM Lasers Support, puts it: “A laser does not cut along a line the way a pen draws one. It removes a strip of material with a measurable width.”
How much material does a cut remove?
There is no universal kerf value. The result depends on the cutting process and the specific setup. For laser cutting, variables include the material, its thickness, focus, lens, power and speed. For abrasive waterjet cutting, OMAX identifies the nozzle, workpiece thickness, mixing-tube wear, and cutting quality and speed as factors.
#1 Best Overall

- UP TO 3X LIFE*
- Optimized Tooth Geometry Designed For Increased Accuracy
- Ultra Sharp Carbide for Clean Cutting
As a contextual example, BRM Lasers gives a typical range of 0.1 to 0.3 mm for CO₂-laser cutting of nonmetals. That is BRM’s stated range, not a specification for every CO₂ laser or material. A separate machine-specific example is Haas’s HAB manual, Revision A, dated October 2025: it specifies 0.07 in (1.8 mm) for the original blade supplied with that machine. Do not use either number as a substitute for measuring your own setup.
Thickness and edge shape matter
A laser cut may be slightly wider at the top face than at the bottom. If a part needs to fit against another, consider which face or depth determines the fit; a single measurement at one surface may not represent the whole cut. For waterjet work, use the material and cutting quality intended for the part when checking kerf, as OMAX recommends.
Rank #2

- Featuring a 10-inch diameter (254 mm), a 5/8-inch arbor (15.88 mm) and a rating of up to 6000 RPM
- Perfect for slicing through both hard and softwoods of all kinds
- Ultra-thin 1/10-inch kerf (2.4 mm) provides clean and efficient cuts
- Designed with 80 carbide-tipped teeth for ultra-fine finish wood cutting
- Compatible with the majority of 10-inch miter saws, jobsite saws, and table saws
Why do laser-cut parts come out the wrong size?
If the laser follows the center of a drawn line without compensation, it removes material on both sides of that line. The retained outside edge therefore moves inward, making an external part smaller than drawn. For an internal feature such as a hole or slot, the cut removes material outside the drawn boundary, making the opening larger than drawn.
This is why two parts designed to fit together may have too much play or may not fit at all. The drawn boundary is not automatically the finished edge: the cut width must be accounted for when the fit is close.
Free tools Windows power users keep installed
One-click scans. No signup required.
Rank #3

- 10 Inch 80-Tooth Ultra Finish Miter / Table Saw Blade, 0.098" Kerf, Wood Cutting with 5/8" Arbor, ATB
- The blades with high-quality thin kerf and plate for fast, durable, smooth cutting, less vibration and noise, and excellent finish
- Made from high-density tungsten carbide for toughness, wear-resistance, and long life
- Compatible with DeWalt, Skil, Metabo, Makita 10 Inch Miter Saws, Table Saws and other Saws
- Ideal for crosscutting oak, pine, melamine, plywood, and moulding.
How do I measure kerf for my material?
- Match the intended job. Use the same cutter, material, stock thickness and operating settings as the production cut. For waterjet cutting, match the cutting quality as well as the material.
- Cut a test pattern. For a laser, make a test containing an outside square and an internal hole or slot. This lets you check both external and internal features.
- Measure the result. Use calipers to compare the finished feature with its drawn size, or use a suitable kerf gauge. BRM describes reading a dedicated kerf gauge; Rayforge describes measuring a square and a hole.
- Record the measurement with its setup. Note the machine, material, thickness and settings alongside the value so you know what it applies to.
- Recheck when the setup or result changes. A value from another material, thickness, focus or power-and-speed combination may not transfer. Recheck if a relevant variable changes or a previously stable cut shifts.
How should I compensate for kerf?
For a laser path centered on the intended boundary, a common correction is to offset the path by half the measured kerf. The direction depends on which side of the line is the retained part:
- External contour: offset outward so the finished outer edge reaches the intended boundary.
- Internal hole or slot: offset inward so the finished opening does not grow beyond the intended boundary.
Software may use its own sign convention or support compensation only for particular geometry. For example, xTool documents kerf offset for closed shapes. Check how the application handles the specific path, then verify the chosen offset with a test cut before relying on it for a close fit.
Rank #4
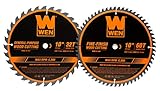
- Featuring both a 32-tooth blade for general woodcutting and a 60-tooth blade for fine-finish woodworking
- Blades measure in at 10-inch diameter (254 mm) with a 5/8-inch arbor (15.88 mm) and a rating of up to 6000 RPM
- Ultra-thin 1/10-inch kerf (2.4 mm) provides clean and efficient cuts
- Perfect for slicing through both hard and softwoods of all kinds
- Compatible with the majority of 10-inch miter saws, jobsite saws, and table saws
What to keep in a kerf record
Kerf is a property of a cutting setup, not just a tool model. Keeping the measured value with the conditions that produced it makes it easier to reproduce a fit later and spot when a changed tool condition or setting calls for another test.
Quick Recap
Best Value

- High-Performance TiCo Carbide - Ensures a sharp and durable cutting edge, designed for both rip cuts and crosscuts in various wood materials.
- Perma-SHIELD Non-Stick Coating - Protects the blade from heat, gumming, and corrosion, extending the blade's life.
- Super Thin Laser Cut Kerf - For fast, durable, and clean cuts, good for your remodeling and demolition needs.
- Tri-Metal Shock Resistant - The brazing allows carbide tips to withstand extreme impact for maximum durability.
- Hardened Steel Body - Provides longevity and consistent performance, maintaining a sharp cutting edge for a wide range of applications.
- Machine and cutter or blade
- Material and thickness
- Relevant settings, such as laser focus, power and speed, or waterjet cutting quality
- Measured kerf and where it was measured through the thickness
- Date and any observed change in tool condition
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.
Quick wins for a faster PC:
Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Clear out junk files and repair common Windows errorsFree Scan →Scan for outdated or missing drivers - takes under a minuteDriver Scan →