Some links on this page are affiliate links: if you buy through them we may earn a commission, at no extra cost to you.
To compare printed ABS with carbon-fiber nylon, test a defined printing process—not just two material names. Control the filament, printer, orientation, specimen geometry, conditioning, and test method; then report the results and how each specimen failed. A coupon can characterize that process, but only a test of the actual part can show whether its geometry and load path meet a construction or engineering requirement.
What destructive testing can—and cannot—tell you
Destructive testing loads a specimen until it deforms or breaks. Depending on the method, it can reveal strength, stiffness, yield, elongation, energy absorbed, and where a crack starts. It can expose defects that a visual check may miss, including voids, under-extrusion, weak layer bonds, delamination, and local fiber clumping. Testing is most useful when it answers a defined question, such as whether a bracket survives a specified load or whether a print orientation improves performance.
A result applies to the material, machine, process settings, specimen, conditioning, and test procedure used to produce it. It is not automatically a design allowable for a different part or printer. ASTM standards provide recognized test methods, but they do not constitute a universal qualification system for every fused-filament-printed polymer part. ASTM identifies polymer additive-manufacturing inspection as an area of ongoing standards work: ASTM WK85121.
Distinguish the material and the purpose of the test
- ABS is an amorphous thermoplastic whose printed performance can depend on interlayer fusion, thermal gradients, cooling, warping, infill, orientation, and post-processing.
- Carbon-fiber nylon is not one universal formulation. It may use nylon 6, nylon 6/6, nylon 12, or another polyamide, usually with chopped fibers. Continuous-carbon-fiber systems are a different reinforcement approach and should not be treated as equivalent to chopped-fiber filament.
- Material characterization compares specimens made by a defined process. Part validation tests the actual geometry under representative loads. Process qualification checks whether a controlled manufacturing process repeatedly produces acceptable parts.
Choose a test that matches the service load
| Service question | Common method | What it can show |
|---|---|---|
| Will the material carry a pulling load? | Tensile; ASTM D638 or ISO 527-2 | Strength, modulus, elongation, and failure behavior |
| Will the part bend? | Three-point flexure; ASTM D790 or ISO 178 | Flexural strength, modulus, and deflection |
| Will a sudden blow cause fracture? | Notched or unnotched Izod impact; ASTM D256 | Impact energy under the specified configuration |
| Will a part be crushed? | Compression test | Crushing, buckling, layer collapse, or other compression failure |
| Will it see repeated or sustained load? | Fatigue or creep testing | Durability under cycling or time under load |
| Will it operate hot or in a harsh environment? | Heat, humidity, chemical, UV, or other exposure followed by mechanical testing | Property changes under the specified exposure |
The standards are related, not interchangeable. Current ASTM committee listings identify D638-22, D790-25, and D256-26 as active editions associated with plastics mechanical-properties work; check the applicable standard and edition before claiming compliance: ASTM D20.10. The linked ASTM store pages for D638 and D256 refer to specific listed editions, so confirm the current applicable edition rather than assuming a store-page link represents the latest one: ASTM D638 listing and ASTM D256 listing. ASTM lists D790-25 here: ASTM D790-25.
#1 Best Overall

- 15% Carbon Fiber Reinforced PA612: Fiberon PA612-CF15 is a long-chain PA612 nylon reinforced with 15 wt% carbon fiber. It combines lower moisture sensitivity than PA6-based nylon with stronger mechanical performance than PA12-based materials, making it suitable for rigid functional parts, tooling, jigs, fixtures, and engineering prototypes.
- Strength Retention After Moisture Exposure: Typical TDS values include 91.9 MPa dry X-Y tensile strength and 83.1 MPa after the specified annealing and moisture-conditioning process. This balance makes the material useful for parts that may experience changing humidity during service.
- Heat Performance After Annealing: The heat deflection temperature reaches 175°C at 0.45 MPa after annealing at 100°C for 16 hours. Annealing also helps improve dimensional stability. HDT is a standardized test value and should not be interpreted as the continuous operating temperature of every printed part.
- Lower Moisture Sensitivity Still Requires Dry Storage: PA612-CF15 is less moisture-sensitive than PA6-based nylon but remains hygroscopic. Keep the filament below 20% relative humidity during storage and printing. Dry at 100°C for 10 hours before use if exposed to ambient humidity or if stringing, bubbles, or rough surfaces appear.
- Advanced Printer and Wear-Resistant Nozzle Required: Use an all-metal hotend, a 250–300°C nozzle, a 40–50°C build plate, and a hardened steel or ruby nozzle with the cooling fan off. A heated chamber is not required under the TDS conditions. Speeds up to 300 mm/s may be possible with a tuned profile. Before long prints, confirm smooth filament routing and unrestricted spool rotation.
Tensile testing
A universal testing machine pulls a specimen until it yields or breaks. A tensile curve can provide strength, modulus, yield stress where applicable, and elongation. ASTM D638 is a common plastic tensile method, but results depend on specimen preparation, test speed, and environment. Instron describes typical D638 test speeds spanning 1 to 500 mm/min, with selection dependent on the material and setup; that range is guidance, not a universal setting: Instron ASTM D638 guide.
Orientation changes what the test measures. Flat specimens are generally loaded in the build plane; edge or upright specimens place raster and layer interfaces differently relative to the load. Include the orientation most representative of the intended part, and test other orientations when anisotropy is important. A high flat-coupon value does not establish safety when the real part carries tension across layer interfaces.
Flexural testing
ASTM D790 uses three-point bending to assess flexural properties of reinforced and unreinforced plastics. It is useful for beams, brackets, covers, clips, and levers whose service load is dominated by bending. Four-point bending, such as ASTM D6272, can be useful when a constant-moment region is needed. Method selection and limitations should be checked against the standard and material behavior; see Instron’s D790 guide.
Quick wins for a faster PC:
Scan for outdated or missing drivers - takes under a minuteDriver Scan →Clear out junk files and repair common Windows errorsFree Scan →Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Flexural strength is not a single, geometry-free measure of material strength. Bending combines tension at one surface, compression at the other, and shear through the specimen; span, depth, loading nose, surface flaws, and layer structure all matter. A printed specimen may fail by delamination or interlayer shear rather than a clean material fracture.
Rank #2

- 【Stiff & Strong & Heat Resistant】 - SUNLU PA6-CF nylon filament 1.75mm is made of 80% PA and 20% Carbon Fibers. The carbon fiber reinforcement really provides significantly improved stiffness, strength and heat resistance with outstanding layer adhesion.
- 【Good for Industrial Engineering Printing】 - SUNLU PA6 CF is very strong, durable and features an excellent heat resistance, the models printed with Carbon Fiber Nylon Filament can be used in many industrial fields. It can be used in applications requiring torsional, tensile, and impact strength. Such as gears, screws, helmets, fan blades, toy car chassis, skateboard parts, bicycle frames, etc.
- 【Heat-Resistant】- PA6 Filament withstands up to 209°C, much higher than Easy PA, PC, ASA and other 3D printing filaments. It can be applied to parts that need to withstand high temperatures, such as automobile exhaust pipes, motor covers, pot handles, the bottom of the kettle, etc.
- 【Not Compatible with AMS】- PA6-CF is too brittle and prone to breaking inside the printer. Not recommended for use with AMS, AMS Lite, or other multi-color systems.
- 【Printing Setting】 - Nozzle: 270-290℃; Bed Temperature: 50-70℃; Speed: 50mm/s – 150mm/s; Annealing: 80℃~130℃ 5-12h (To ensure a good heat resistance of your printed part it is recommended to anneal your print model); Bed Surface: almost any surface with a thin coat of PVA glue or Magigoo PA.
Impact, compression, fatigue, and creep
ASTM D256 Izod testing uses a pendulum to break a notched or unnotched specimen under defined conditions. It answers a different question from a slower tensile test. Record notch condition and orientation, temperature, conditioning, pendulum energy, and whether the specimen breaks completely. Do not compare impact values from different standards or configurations as if they were equivalent: ASTM D256 listing.
Compression testing is relevant to spacers, feet, bushings, fixtures, and columns. Watch for buckling in slender specimens, which can obscure material behavior, as well as barreling, crushing, layer collapse, fiber-direction splitting, and infill collapse. Repeated loading calls for fatigue testing; sustained load calls for creep testing. Add heat, humidity, water, chemical, UV, or freeze-thaw exposure when those conditions are part of service. Nylon moisture state must be defined because a dry specimen and a moisture-conditioned specimen are not directly comparable.
Build a fair, reproducible test plan
1. Write down the engineering question
Examples include: which process makes a bracket withstand a specified load; whether upright printing reduces capacity; whether annealing changes a required property; or how much performance changes after humidity exposure. A test that is not tied to a question can produce numbers without guiding a decision.
2. Lock the print variables
Record the printer model and firmware; filament maker, exact product, and lot if available; nozzle type and diameter; filament age and storage; drying procedure; nozzle, bed, and chamber temperatures; layer height and line width; perimeters and top/bottom layers; infill percentage and pattern; raster; speed and cooling; support and removal method; build orientation; post-processing; and time from printing to testing. Do not call a cross-printer comparison a material-only comparison unless that process difference is explicit.
Rank #3
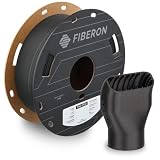
- 20% Carbon Fiber Reinforced PA6: Fiberon PA6-CF20 combines Nylon 6 with 20% carbon fiber for high stiffness, strength, dimensional stability, and strong layer adhesion. Designed for rigid functional parts, tooling, fixtures, and automotive or industrial prototypes.
- Engineering Performance After Annealing: Typical TDS values include 109.3 MPa dry X-Y tensile strength and an 8.64 GPa Young’s modulus. Heat deflection temperature reaches 215°C at 0.45 MPa after annealing at 100°C for 16 hours. Final-part performance may vary with design and printing conditions.
- Dry Before and During Printing: PA6 is moisture-sensitive. Dry the filament at 100°C for 10 hours before printing, then store and print below 20% relative humidity, ideally from a dry box. Proper moisture control helps reduce stringing, bubbles, rough surfaces, and inconsistent extrusion.
- Advanced Printer Setup Required: Use a 280–300°C nozzle, a 40–50°C build plate, and an all-metal hotend with the cooling fan off. A heated chamber is not required; room-temperature chamber conditions are listed in the TDS. Printing speeds up to 300 mm/s are possible with a properly tuned profile.
- Use a Wear-Resistant Nozzle: Carbon fiber is abrasive, so a hardened steel or ruby nozzle is required instead of a standard brass nozzle. For optimum heat resistance and dimensional stability, anneal printed parts at 100°C for 16 hours. Before long prints, confirm smooth filament routing and unrestricted spool rotation.
“100% infill” does not guarantee a void-free, uniform specimen. Line width, perimeter count, overlap, extrusion, slicer behavior, and skin structure can all affect the result.
3. Define conditioning and post-processing
Label specimens as-printed, dried, humidity-conditioned, water-exposed, or annealed, and document the actual procedure and elapsed time. Nylon is moisture-sensitive; ABS results can also shift with thermal history and residual stress. UltiMaker’s Nylon CF sheet reports different properties by printed orientation and distinguishes annealed from non-annealed conditions, illustrating why those details belong beside any quoted value: UltiMaker Nylon CF technical data sheet.
4. Print replicates and vary factors deliberately
One specimen is an anecdote, not a robust comparison. Print multiple specimens per condition so you can report scatter and identify invalid tests. A Stratasys comparison of ABS-CF10 and Nylon-CF10 tested 10 specimens per material and toolpath type across tensile, flexural, and impact procedures; that is an example of replication, not a universal required count: Stratasys study.
The Tool Desk
Outbyte Driver Updater FREEScan for outdated or missing drivers - takes under a minuteDriver Scan →Outbyte PC Repair FREEClear out junk files and repair common Windows errorsFree Scan →A manageable first comparison might hold print settings constant while varying material and orientation. A later study can add raster, infill, perimeters, moisture condition, or annealing. Avoid changing many factors at once unless the experiment is designed to separate their effects.
Rank #4

- 1. Tips: (1) Nozzle Temp: 260 - 280 ℃ (2) Hotbed Temp: 90 - 100 ℃ (3) Printing Speed: <200 mm/s (4) We recommend using a closed-type printer. (5) Printing have emit odors. Please ensure adequate ventilation, preferably with an exhaust fan.
- 2. Carbon Fiber Reinforced Industrial Performance Blended with premium carbon fiber, this ABS-CF filament higher stiffness and greater tensile strength than standard ABS, perfect for load-bearing functional parts, jigs, fixtures and industrial end-use components.
- 3. Minimal Warpage & Outstanding Dimensional Stability Engineered to solve ABS’s common warping/shrinking issues, our filament ensures tight dimensional accuracy ±0.03mm, strong interlayer bonding, and consistent printing results for complex structural models.
- 4. Lightweight & Premium Matte Finish High strength-to-weight ratio reduces part weight without compromising rigidity; prints smooth matte carbon fiber texture, no post-processing needed for professional-looking prototypes.
- 5. Wide Compatibility & Ready to Print 1.75mm diameter, 1kg/2.2lbs vacuum-sealed spool with desiccant, compatible with most enclosed FDM 3D printers.
5. Inspect and measure before loading
- Photograph and label each specimen, including its build and raster orientation.
- Measure gauge width and thickness with suitable tools; for flexural coupons, record repeated width and thickness readings and use the mean dimensions as appropriate to the method.
- Record warping, visible voids, surface defects, and mass if density consistency matters.
- Decide in advance how visibly defective specimens will be handled; do not silently discard failures that could be part of the process variation.
6. Match equipment and fixtures to the test
A tensile or compression frame needs appropriate capacity, a calibrated load cell, suitable grips, and data capture. Tensile strain measurement may require an extensometer or non-contact system. Flexure needs a correctly configured fixture; quantitative impact work needs a calibrated pendulum tester rather than an improvised drop test. Instron notes that 5 kN or 10 kN systems are common for many plastic tests, while high-strength reinforced plastics may need 30 kN or 50 kN systems. These are examples, not sizing rules: choose capacity from expected load, specimen geometry, fixtures, and safe operating margin. See the Instron D638 guide.
7. Test the production part as well as coupons
A standard dog-bone coupon cannot reveal whether a bracket fails at a fillet, bolt hole, boss, thin wall, or layer transition. For part validation, reproduce the actual geometry, fasteners and inserts, contact surfaces, mounting, service orientation, temperature, loading rate, and expected load spectrum. Define the acceptance criterion and safety factor for the application rather than converting a coupon strength into a claimed load rating.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.Read the failure, not just the peak number
Maximum load alone is incomplete. Preserve the load-displacement curve and record the maximum load, displacement at that load, and energy to failure when relevant. Classify the failure location and mode:
- Ductile necking or stretching: substantial deformation before rupture, potentially seen in ABS depending on formulation and process.
- Brittle or semi-brittle fracture: limited deformation before break; possible in filled composites depending on material and configuration.
- Layer separation or delamination: failure along printed interfaces, indicating that orientation or bonding may be controlling.
- Fiber pullout or breakage: evidence of reinforcement behavior, but not by itself proof of good overall interlayer strength.
- Grip failure or slip: a tensile result that did not fail in the intended gauge section should not be treated as a valid material failure.
- Buckling or infill collapse: may govern compression behavior, especially in slender or internally structured specimens.
Photograph specimens before and after testing and, where useful, inspect fracture surfaces under magnification. A crack starting at a void or notch has a different engineering implication from a clean gauge-section break. Use shielding and eye protection, secure fixtures, and handle broken fiber-filled specimens carefully; fragments and cutting or fracture debris can be sharp.
Best Value

- High Strength and RigidityHigh Strength and Rigidity: Incorporates 15% short carbon fibers, significantly enhancing tensile strength and rigidity. Maintains structural stability under high loads or stress, with minimal deformation.: Incorporates 15% short carbon fibers, significantly enhancing tensile strength and rigidity. Maintains structural stability under high loads or stress, with minimal deformation.
- Heat Resistance and Dimensional Stability: Delivers exceptional mechanical performance and dimensional stability even under high temperatures. Reduces the risk of material fatigue and deformation for parts exposed to prolonged high-temperature conditions.
- Lightweight Design: Thanks to the low-density properties of carbon fiber, printed parts achieve both high strength and lightweight characteristics. Ideal for aerospace and automotive applications, effectively reducing weight while improving overall performance.
- Superior Chemical Resistance: Resistant to various chemicals, including acids, alkalis, oils, and solvents. Ensures long-lasting durability and reliability even in harsh industrial environments.
- Versatile Applications: Widely applicable in automotive components, mechanical fixtures, electronic device mounts, and aerospace structures. Excels in both prototyping and end-use scenarios, offering outstanding mechanical properties and thermal stability.
Report results so another engineer can interpret them
For each condition, report the exact material and process alongside the method and outcome. Include the number of valid specimens and mean, standard deviation, minimum, and maximum; retain invalid runs and explain why they were excluded. A concise report should contain:
- Tensile: strength, modulus, yield if defined, elongation at break, speed, orientation, conditioning, and failure-mode distribution.
- Flexural: strength, modulus, load and deflection, specimen dimensions, span, speed, and whether the sample broke, yielded, or reached a strain limit.
- Impact: energy, notch configuration, orientation, temperature, conditioning, and complete or partial fracture.
- All tests: printer and material identification, print settings, post-processing, test date, equipment and calibration status, and specimen photographs.
Do not treat ASTM D638 and ISO 527-2, or ASTM D790 and ISO 178, as interchangeable. Instron notes differences in specimen dimensions, calculations, and test-rate requirements between these related methods: D638 and ISO 527-2 guidance and D790 and ISO 178 guidance. Likewise, do not compare tensile strength with flexural strength, dry nylon with humid nylon, a favorable flat coupon with an upright one, or chopped-fiber nylon with continuous-fiber composite data as though the figures describe the same test condition.
Use data sheets carefully when comparing ABS and CF nylon
Manufacturer data are useful for screening, but they describe particular products and test conditions—not every print or application. UltiMaker’s Nylon CF data are orientation-specific. CarbonX’s PA6-CF information identifies printed conditions such as 100% infill and ±45° raster and warns that its values should not alone establish design specifications: CarbonX PA6-CF Gen 3 information.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
Check the resin, fiber form and content, specimen orientation, infill, raster, machine, conditioning, and post-processing before using a published number. One commercial example also illustrates why test-method labels deserve scrutiny: the MakerBot Method ABS-CF page labels some tensile and heat-deflection entries with ASTM D648, a method associated with heat-deflection temperature. Verify those entries with the manufacturer before treating them as authoritative: MakerBot Method ABS-CF product page.
What each material may suit
- ABS: consider it when a relatively tough, familiar thermoplastic, lower material cost, or easier finishing is valuable and very high stiffness is not the priority. These are selection considerations, not guaranteed properties for every ABS formulation or printed geometry.
- Carbon-fiber nylon: consider it when stiffness, strength-to-weight potential, or dimensional stability in a suitable formulation and direction matters. Plan for moisture control, possible reduced ductility or notch sensitivity, abrasive nozzle wear, and more demanding processing. Chopped-fiber reinforcement does not make every direction strong or every part tough.
For example, the ELEGOO PAHT-CF product page recommends a hardened-steel nozzle and drying at 80 °C for 8 hours before use; treat those as that product’s vendor instructions, not as a universal recipe for all CF nylon: ELEGOO PAHT-CF product page.
When an in-house test is enough—and when it is not
A controlled in-house comparison can help with early design choices and process troubleshooting if the equipment, fixtures, specimen preparation, and reporting are consistent. Use a qualified materials laboratory when results must support product certification, customer acceptance, regulatory submissions, safety-critical design, formal material qualification, or traceable accredited reporting. A lab can help select the method and document calibration and conditioning; a machine’s presence alone does not establish standards compliance. Commercial testing systems and fixtures are described by Instron plastics testing.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.
Leave a Reply